Project brief from a Durban stainless shop
The client is a stainless component producer in Durban making repeated contour parts for local industrial buyers and maintenance contractors. Their work involved continuous edge finishing, profiling and slotting on CNC machining centres, with parts running through day and night shifts. The main issue was inconsistant tool wear. One batch would cut cleanly, then the next would show early edge breakdown, poor surface finish and more operator adjustments.
The brief was straightforward. Improve tool life on repeated contour milling, keep dimensions stable across batches, and reduce the time spent changing tools mid-job. They also wanted a cleaner result on stainless that can work harden fast if the chip load is wrong or the cutter dwells for too long.
Constraints on the floor in Durban
The job was not just about the cutter. The workshop was dealing with coastal humidity, variable shift patterns and the usual pressure that comes with load-shedding backup planning. The machine operators needed tools that held up under production use without constant tweaking. The parts also had narrow radii and repeated contours, so any chatter or heat build-up showed up quickly on the finish.
- Material: stainless steel component work, repeated contour milling and finish passes
- Machine type: CNC machining centres used in production batches
- Key risks: heat build-up, edge wear, burrs and finish marks
- Operating pressure: limited downtime between shifts and urgent repeat orders
Because the components were repeated often, the client also wanted a more predictable tool plan. That meant fewer surprises from batch to batch and better control over stock on hand.
Tool package supplied for the trial
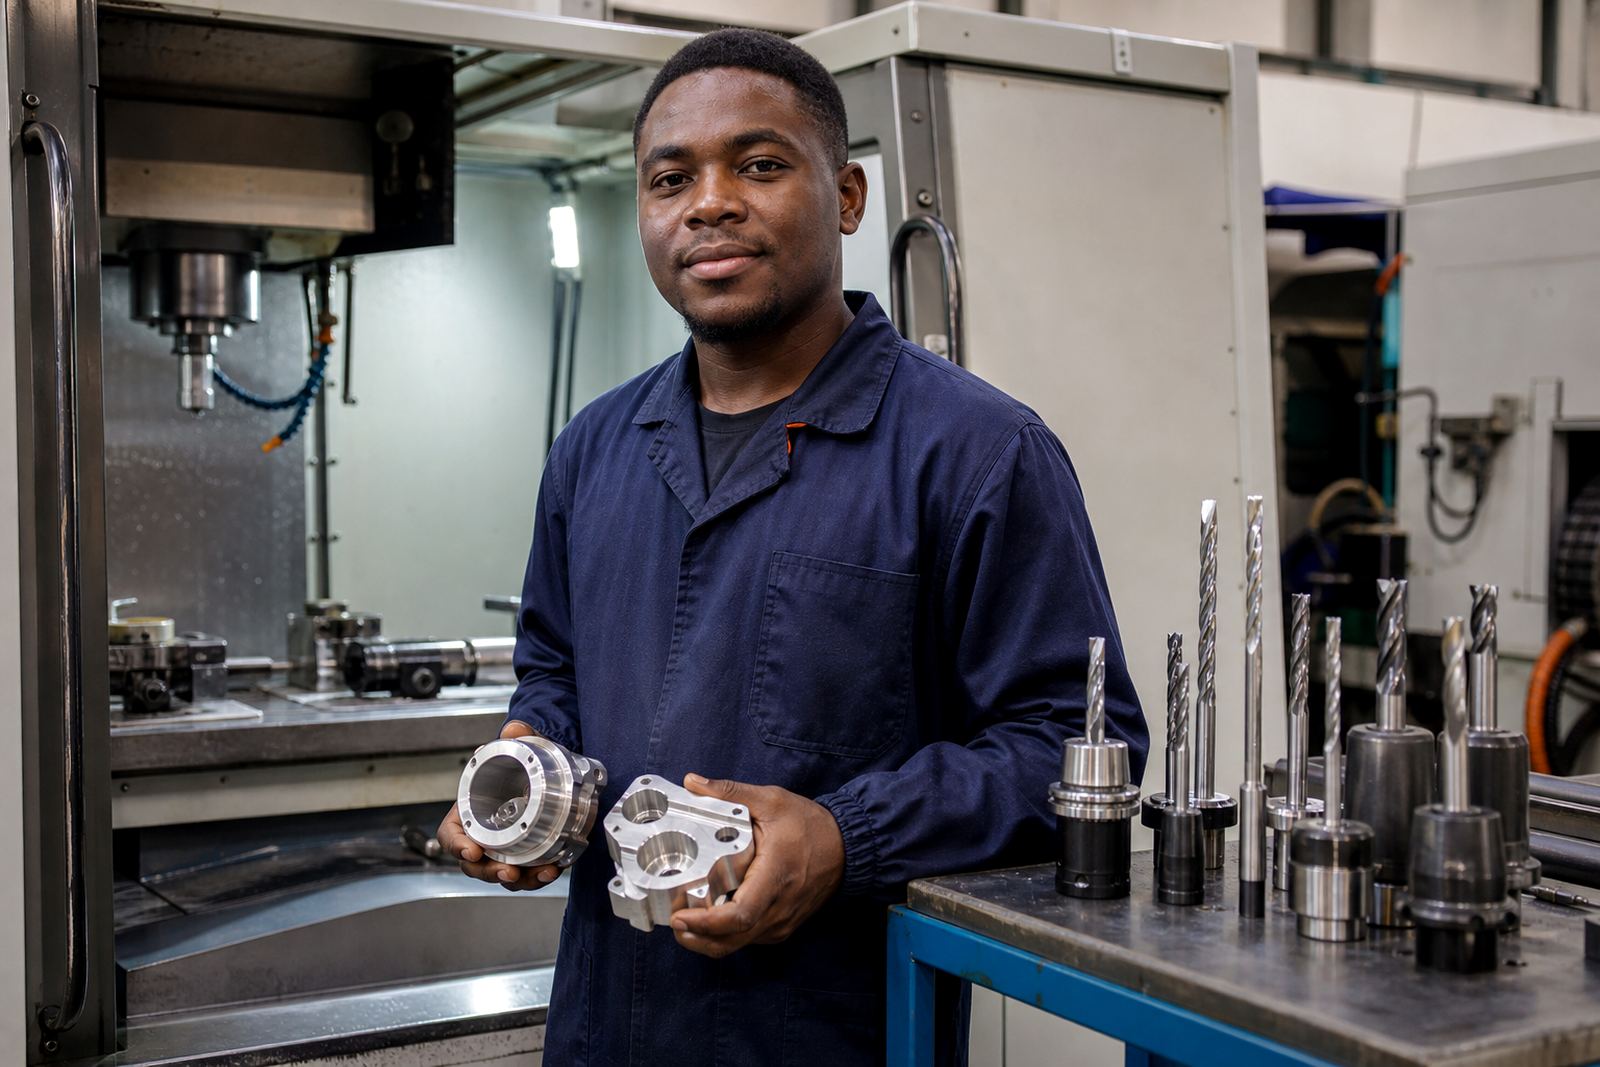
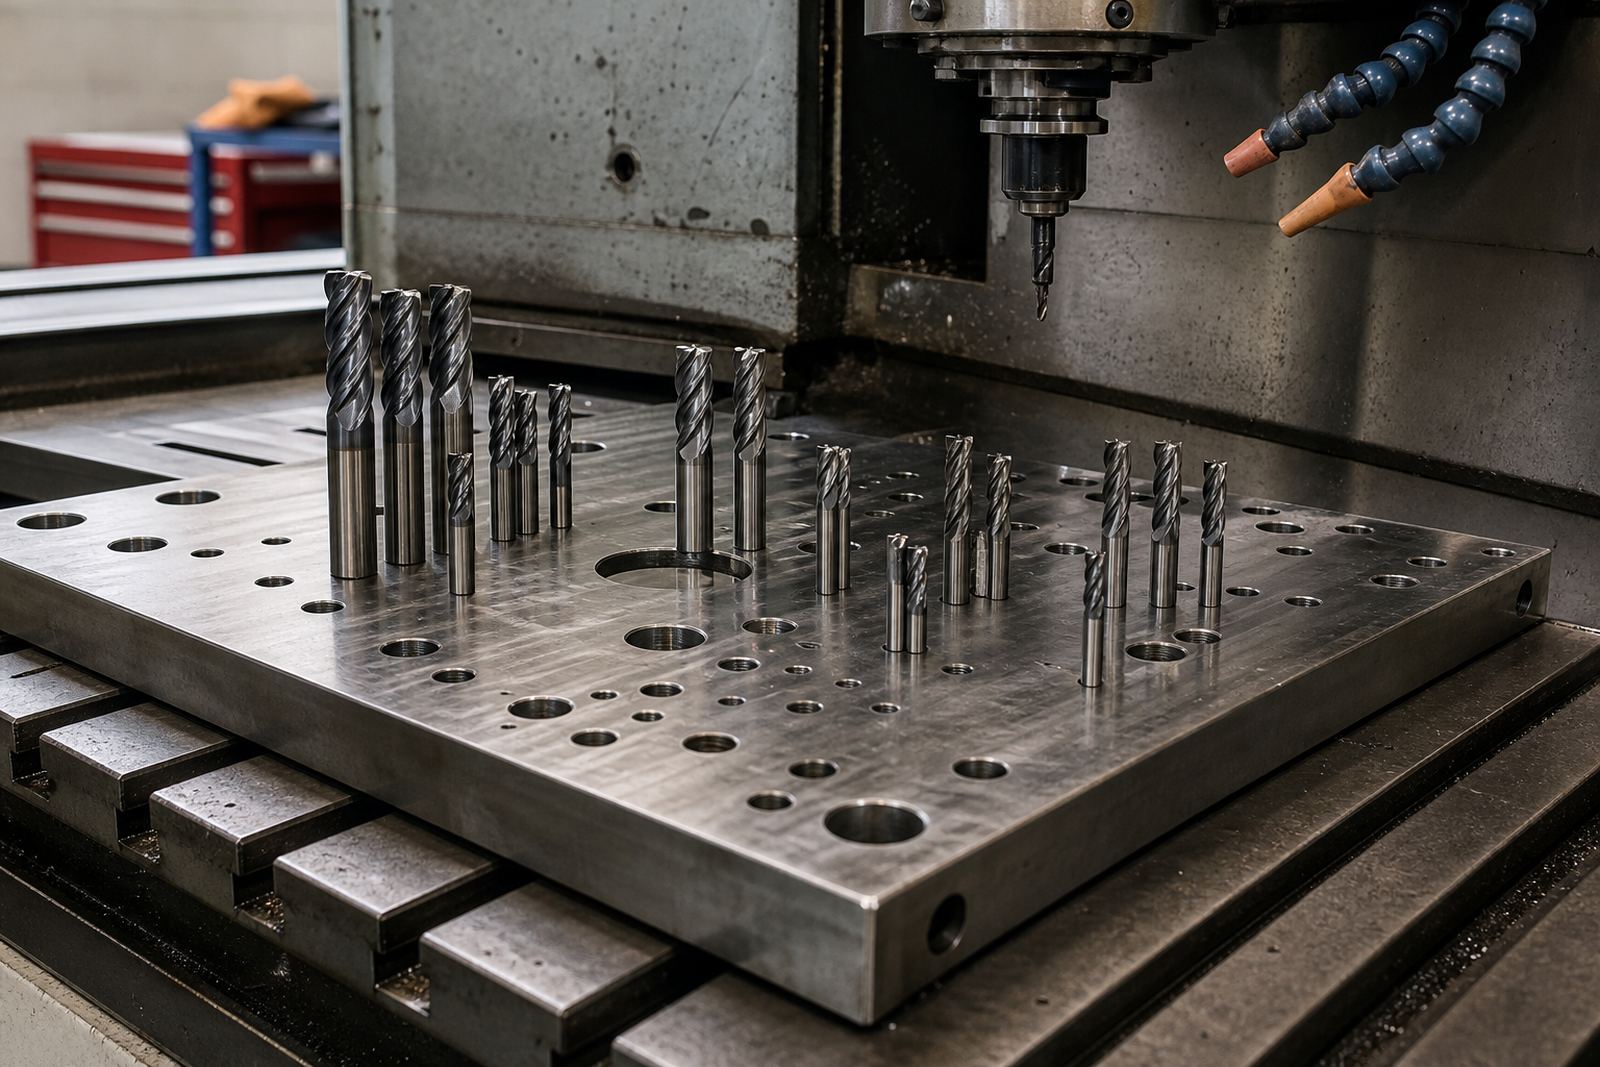
We put together a trial package of solid carbide end mills and drills suited to stainless work, with the sizes chosen around the part features and the machine envelope. The cutters were selected for stable cutting in 304 and similar grades, where the edge has to stay sharp and the chip evacuation needs to be clean. For the tighter contour sections, we prioritised smaller diameter end mills with good rigidity. For holemaking, we matched drill geometry to the material and spindle conditions rather than using one general setting across the board.
- Solid carbide end mills for contour milling and finishing
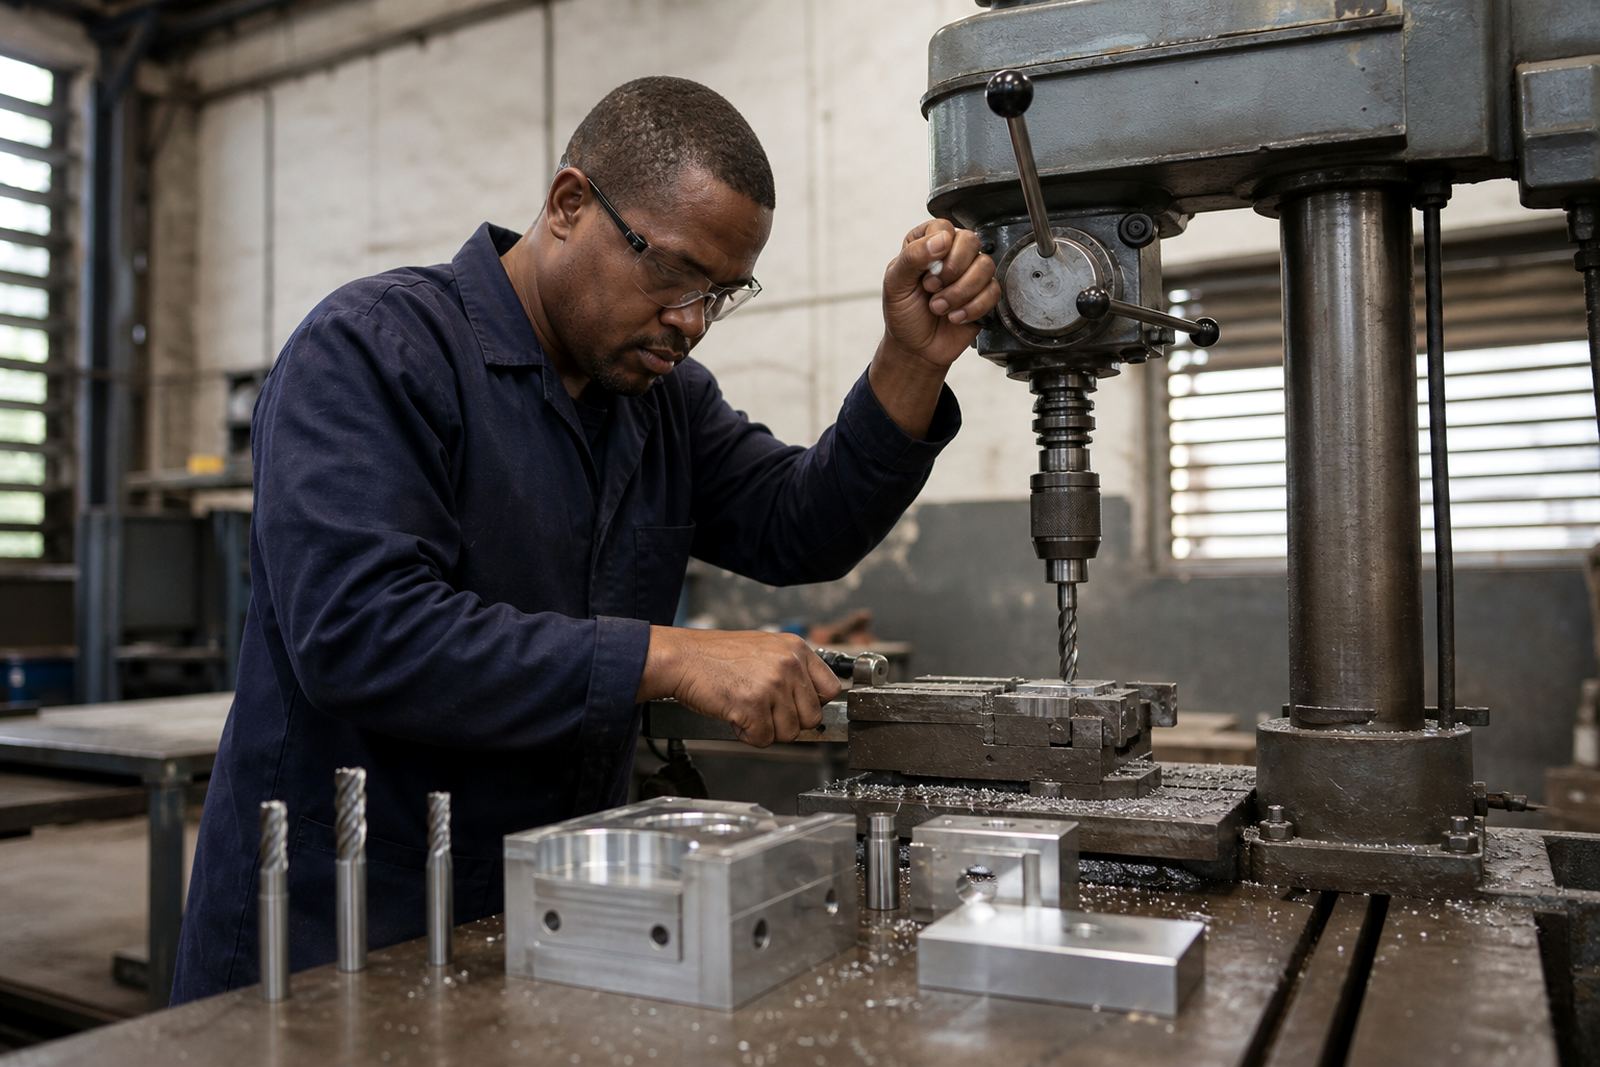
- Solid carbide drills for repeat hole production
- Speed and feed advice for stainless grades
- Tool life monitoring and process notes during trial runs
We also supplied technical quotations so the team could compare the trial against their existing tool cost per part. That helped the buyer see the difference between purchase price and actual running cost over a production week.
How we handled the first two weeks
The first stage ran over two weeks. Week one covered tool selection, application checks and a small sample run on the machine. We reviewed cutting parameters, chip colour, sound and finish quality. The second week was used to confirm repeatability on the same contour parts, using the same tooling across more than one shift. This was important because a tool that looks fine on one run can behave differently once heat and operator handover are involved.
Johan Smit worked through the speed and feed settings with the production team, while Anele Dlamini and Thabo Molefe helped keep the stock flow organised so the right tools were on hand when needed. Priya Naidoo handled the follow-up on part numbers and reorder planning, and Zanele Khumalo checked that the tools supplied matched the requested sizes and tolerances. It kept the process tight and practical, with no wasted time on the shop floor.
What changed on the machine
After the new tooling was introduced and the settings were tightened up, the client saw steadier tool life on repeated contour milling. The cutters held their edge more evenly, and the finish stayed more consistent across batches. There was less chatter on the tighter curves and less time spent cleaning up edges after machining. Tool changes dropped as well, which helped on the longer shifts where one interrupted job can slow the whole line.
- More stable tool life across repeat runs
- Better surface finish on contour sections
- Fewer mid-job tool changes
- Less variation between shifts
The production team also had a better base line for future jobs. Instead of guessing at feeds and speeds for each repeat order, they could keep to a known setting and adjust from there only when the material batch changed.
What we would repeat on the next stainless order
If we were setting up the same Durban job again, we would follow the same approach: match the cutter to the actual stainless grade, keep the tool range tight, and verify the first run before scaling up. That is especially important on coastal jobs where humidity, machine condition and shift handover can all affect the final result. We would also keep a clearer stock plan for the most used end mills and drills so urgent repeat work does not wait for an incoming order.
This project showed that steady results usually come from a practical setup, not from chasing one setting for every part. With the right solid carbide tooling, the client got cleaner cutting and more predictable output on a job that had previously been giving them uneven tool life.
- Keep repeat sizes on hand for fast replenishment
- Review feeds after any material change
- Track tool life per batch, not just per shift
- Use sample trials before full production release
Key facts
| Client type | Stainless component producer in Durban |
|---|---|
| Project focus | More stable tool life on repeated contour milling |
| Tools supplied | Solid carbide end mills and drills |
| Timeline | 2 weeks from first trial to repeat confirmation |
| Main result | Less variation between batches and fewer tool changes |
| Service areas | Durban, Johannesburg, Pretoria, Cape Town, Gqeberha and surrounding production hubs |