

Kempton Park Engineering
Home / Projects / Kempton Park Engineering

Projects

Kempton Park Engineering

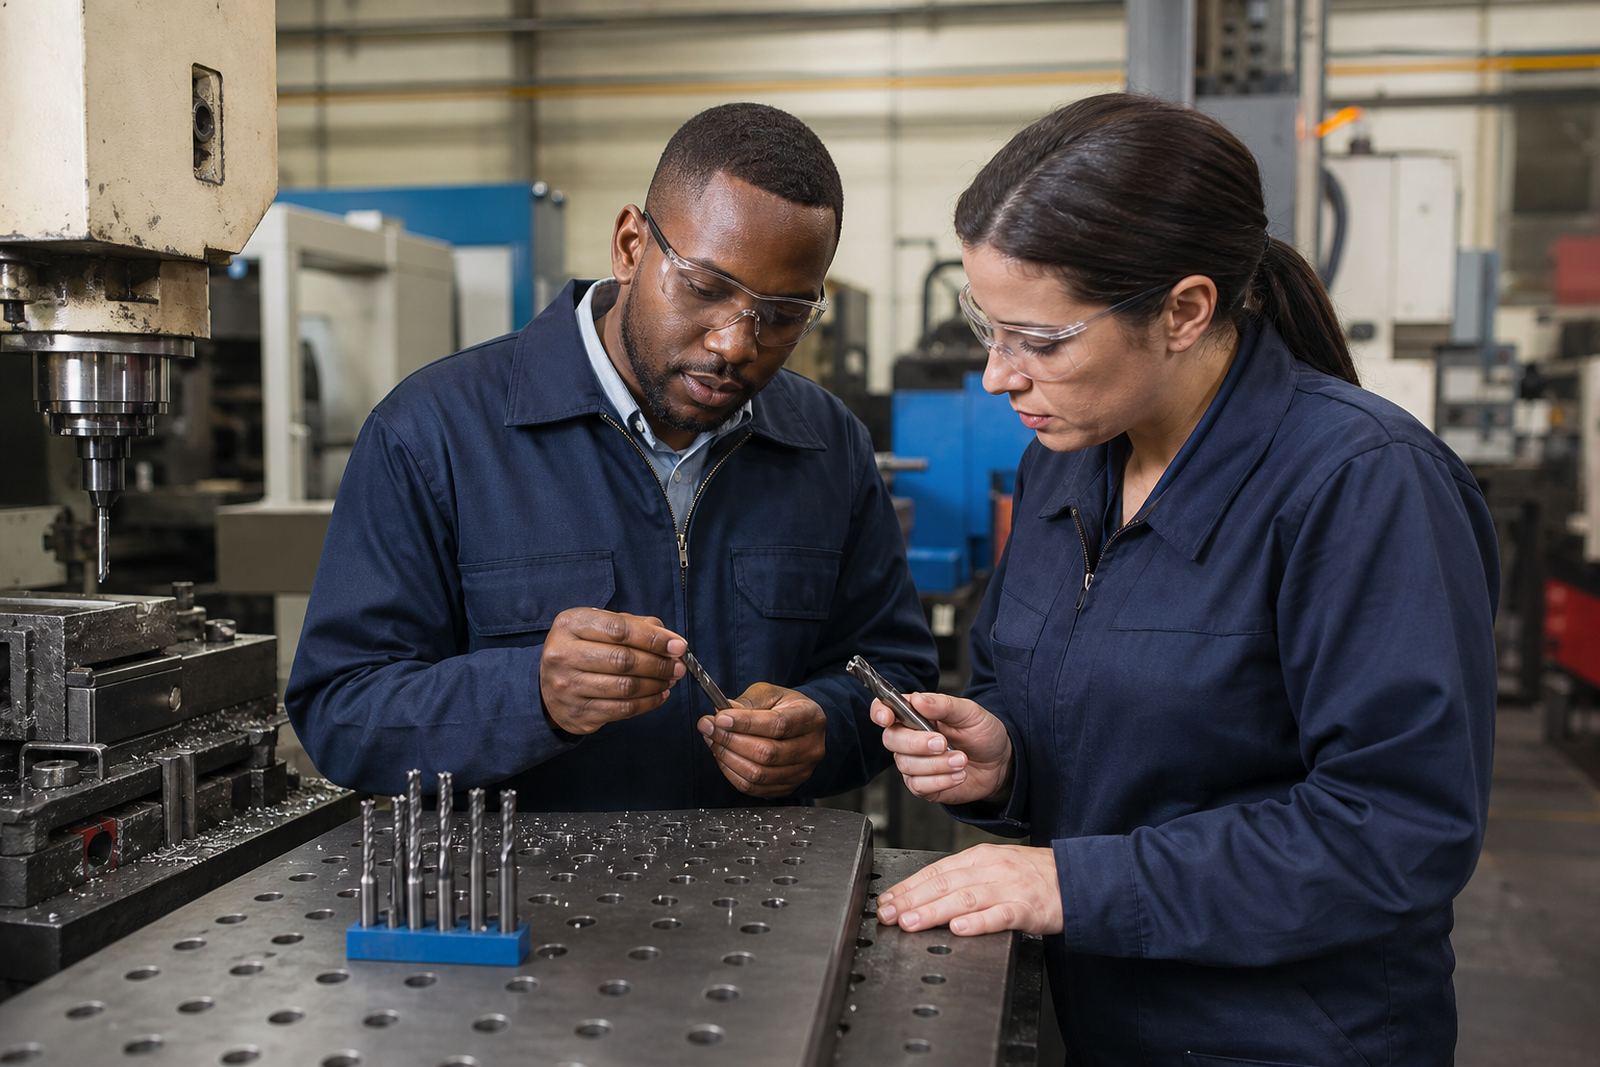
A Kempton Park general engineering shop needed cleaner starts and more predictable hole size on repeated CNC runs. We helped them standardise solid carbide drills, tighten the process, and cut down on rework during production.

The Kempton Park brief: cleaner starts, less rework

The client is a general engineering workshop in Kempton Park making mixed batches for local industry, with work moving between short runs and repeat parts. Their main problem was not a lack of machine capacity, but inconsistency at the drilling stage. Some holes were starting cleanly, others wandered slightly on entry, and tool life was changing too much from one batch to the next.

They asked us to standardise the drill range on CNC machining centres so the team could get cleaner starts, more predictable hole size and fewer offsets during setting up. The job had to suit ordinary day-to-day production, not just one ideal part. That meant selecting drills that could handle mild steel, stainless sections and occasional tougher material, while still giving stable results on long shifts.

The workshop also wanted a supply plan that would work in Kempton Park conditions. Dust, coolant carryover and stop-start work during load-shedding all affect tool performance, so the solution needed to be practical, not fussy.

What was holding the process back

Before the change, the shop was using a mixed set of drills from different suppliers and sizes. That gave them variable point geometry, different cutting behaviour and uneven wear patterns. On some machines the drill would cut well for a while, then suddenly produce rough entry marks or slight oversize holes. The team was compensating with extra spotting, slower feeds, and more manual checks than they wanted.

They also had pressure to keep stock on hand without overbuying. A lot of their work is jobbing work, so tying up too much money in tooling is never ideal. They needed a short list of standard sizes, sensible stock planning, and support that could respond quickly when a tool performed differently in a real part.

  • Mixed drill brands were creating variation between batches
  • Hole starts were not consistent across materials
  • Tool wear was harder to predict on busy shifts
  • Extra spotting and rework added time
  • Stock levels were not matched to actual usage

Our tool selection and setup approach

We reviewed the part mix, machine type, spindle condition and the materials being cut. From there, we proposed a standard set of solid carbide end mills and drills with emphasis on drill entry control, chip evacuation and repeatability. For this project the focus was on solid carbide drills rather than a broad mixed tool list, because the shop wanted one drilling standard they could trust.

We supplied precision solid carbide drills in the sizes most used on the shop floor, including common diameters from 3 mm to 12 mm, with longer sizes for deeper holes where required. The selected drills had a polished flute form for better chip flow, a point geometry suited to cleaner starting, and sizing that supported tighter hole control on CNC machining centres. We also matched the tool choice to the material rather than forcing one drill to do every job.

Johan Smit worked through the speed and feed advice with the operators, while Lerato Mokoena handled the supply side and stock plan. We kept the advice practical, because in a busy Gauteng workshop a good tool still needs a workable set-up on the machine that week, not next month.

  • Solid carbide drill range standardised by diameter and application
  • Point geometry selected for cleaner starts and steadier hole size
  • Cutting data adjusted for each material group
  • Stock planning based on actual monthly use
  • Clear replacement points set for worn tools

Timeline from first review to production use

The project took three weeks from the first enquiry to full use on the shop floor. In week one we reviewed the parts, the drill history, and the most common failure points. In week two we supplied the first trial batch and gave speed and feed guidance for the main jobs. In week three we followed up on performance, checked the hole finish and fine-tuned the tool plan for repeat work.

The quick turnaround mattered because the client had several jobs already booked. They could not stop production for a long testing phase, so the trial had to slot into real work. That is often the case in Kempton Park and the wider East Rand, where a shop may be handling urgent orders, supplier delays and machine time all in the same week.

Results on the machine floor

Once the drills were standardised, the team saw cleaner hole starts and more stable hole size across repeat parts. They also reduced the amount of correction work at the machine, because the drills entered more predictably and held their cutting behaviour better over the batch. Tool changes became easier to schedule, and operators had a clearer idea of when a drill should come out of service.

The biggest gain was consistency. The workshop no longer had to keep guessing which drill would behave differently from the rest. Their setting-up became simpler, and the first-off parts were easier to approve. On a practical level, that helped them keep jobs moving even when the power situation interrupted the day or the workload shifted suddenly.

  • Cleaner starts on repeat drilling operations
  • More predictable hole size across batches
  • Less rework and fewer manual corrections
  • Improved tool life tracking for planning
  • Shorter setting-up time for repeat jobs

What we would repeat for a similar shop

For a similar engineering shop in Kempton Park, Benoni or Germiston, we would do the same core steps again. Start with the part mix, choose the drill range around the real materials, and keep the stock list tight enough to control cost but broad enough to avoid delays. If the workshop runs stainless, mild steel and occasional harder sections, it is better to separate those jobs properly than to push one drill too far.

We would also keep the support close to the floor. A good outcome depends on the right tool, but also on the feed, spindle speed, coolant delivery and chip clearing. Where the machine room is busy or the environment is humid, that detail matters. In coastal work it matters even more, but even inland a workshop can lose time if cutting data is not matched to the job.

For this client, the combination of standardised solid carbide drills, practical application support and a sensible stock plan gave them a repeatable process they could carry forward. The result was not flashy, just more dependable, which is what most engineering shops actually need.

Key facts

Client typeGeneral engineering workshop
TownKempton Park, Gauteng
Project timeline3 weeks
Main product suppliedSolid carbide drills
Key sizes3 mm to 12 mm, with longer options where required
Main outcomeCleaner starts and more predictable hole size

What our Carbide Tooling customers say

Verified Google reviews

Questions we get asked

What was the main problem on this Kempton Park project?

The shop needed cleaner drill starts and more predictable hole size on repeat CNC work. Their mixed tooling was causing variation between batches.

Did you only supply drills for this job?

The focus was on solid carbide drills, but we also helped with tool selection, speed and feed advice, stock planning and follow-up support.

How fast can you respond to a similar request?

For standard stock items we can often move quickly, and urgent requirements are handled through the enquiry process on our contact page.

Planning something? Send the team a message.

Contact form