Starting parameters that suit your machine and material
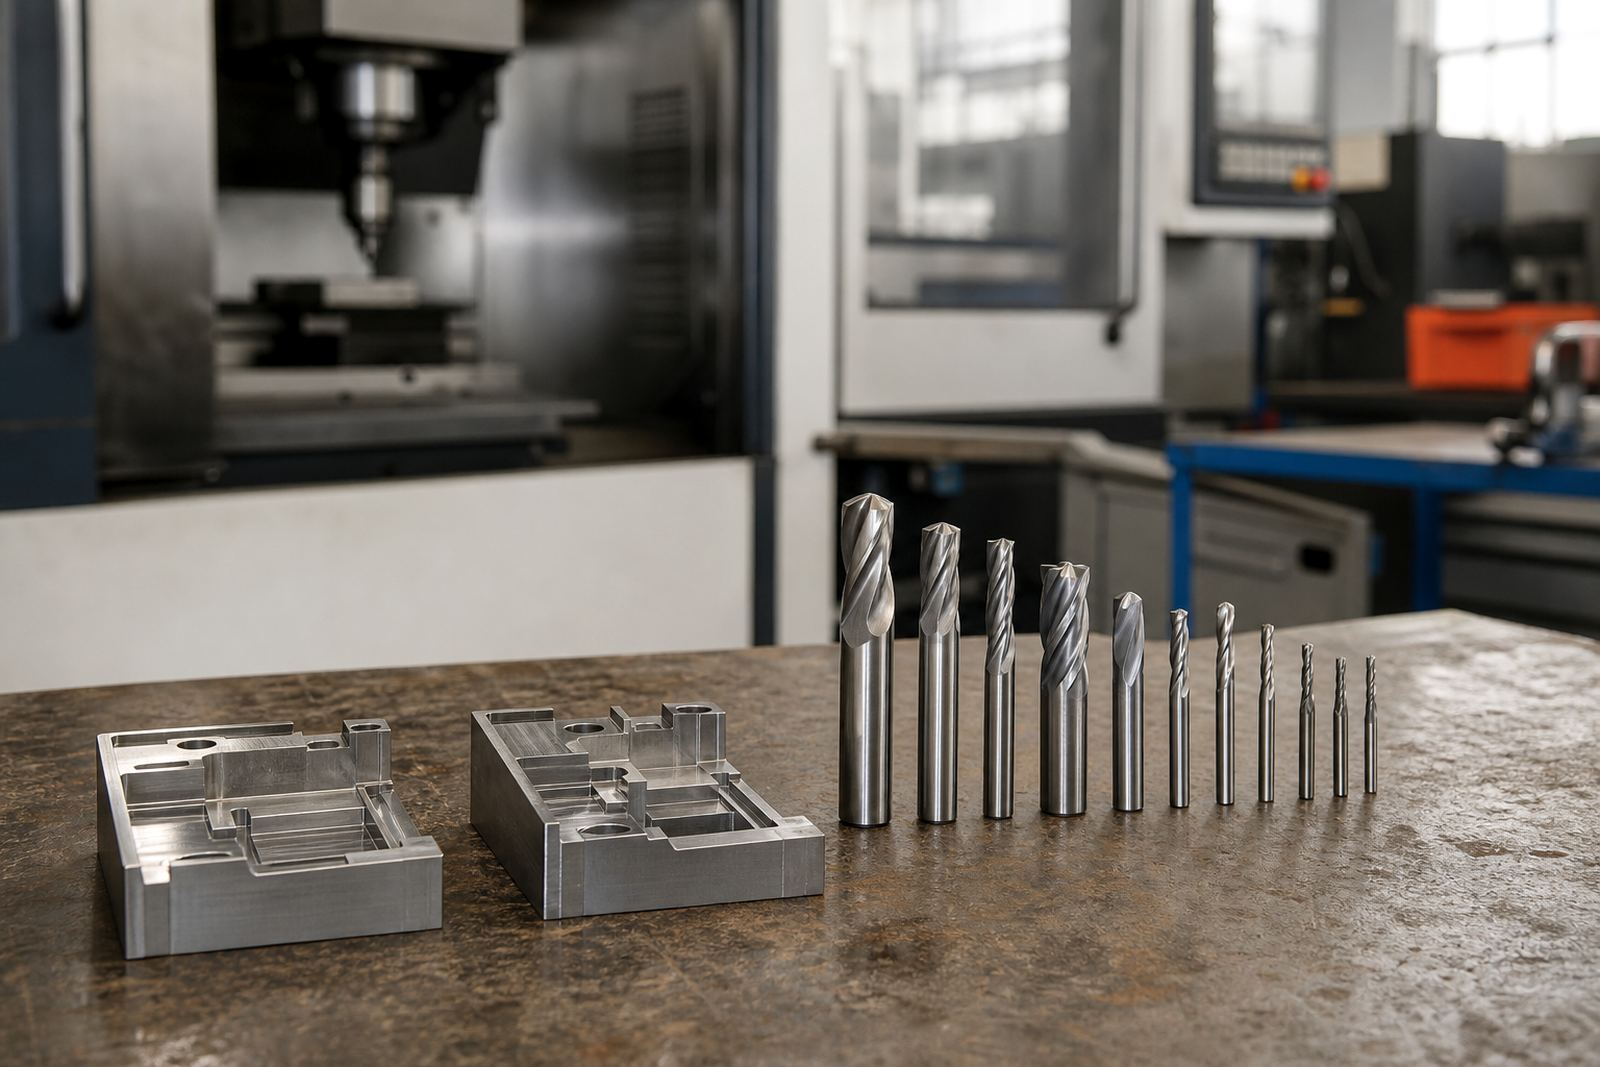
Speed feed advice starts with the basics, not guesswork. We look at the cutter type, flute count, diameter, stick-out, holder, spindle range and the material being machined so the first cuts are sensible and safe. That includes mild steel, tool steel, stainless, aluminium, cast iron and tough alloys used in South African production shops.
For smaller production runs and repeat work, the aim is to reduce chatter, edge breakdown and excess heat while still holding cycle time to a practical level. We help with starting surface speed, chip load, depth of cut and step-over so your operator can make the first setup with confidence instead of wasting time on trial and error.
- Recommended starting RPM and feed rate
- Depth of cut and step-over guidance
- Slotting, ramping and plunge advice
- Notes for coolant, air blast or dry cutting
What is included in the advice session
Each request is handled around the actual job, not a generic chart. We can work from drawings, existing tool lists, machine details and photos of the part or setup. If you are machining on a vertical machining centre, CNC mill or drill-and-tap machine, we can advise on safer entry values and where to make controlled changes.
Where useful, we also flag issues that shorten tool life, such as too much reach, poor clamping, heavy radial engagement or the wrong coating for the material. In coastal areas like Durban and Gqeberha, storage and handling matter too, because humidity can affect tool condition and corrosion risk if stock is left open or packed badly.
- Tool selection for the intended cut
- Starting parameters for milling and drilling
- Tool life saving changes for real production conditions
- Advice for coolant use, chip evacuation and heat control
How we work from enquiry to workable settings
You send through the part details on the contact page enquiry form, including machine type, material, tool size and the issue you want to solve. We then review the application and suggest starting values, plus any changes that will help the tool cut cleaner and last longer. If the job is urgent, we prioritise the response so your shop can get moving again.
When needed, we can also support a sample tool trial and compare the result against the target finish, cycle time and tool wear. This is useful for Gauteng shops dealing with mixed batches, load-shedding interruptions and start stop production, where settings often need to be practical rather than ideal on paper.
- Submit the enquiry form with job details
- We review material, machine and tool data
- Receive starting parameters and notes
- Test, adjust and feed back the result
Turnaround for standard and urgent requests
Most standard advice requests are turned around quickly, usually within the same working day when the details are complete. More complex work, such as multi-operation parts or difficult materials, may take longer if we need to check the tooling sequence and chip control properly. The better the information, the faster we can give you numbers that make sense.
For urgent tool supply and production stoppages, we can also support the setup conversation around immediate replacement tools and practical starting values. That helps shops in Johannesburg, Pretoria, Boksburg, Alberton and Centurion get a machine back into production without running a cutter too hard on the first pass.
- Same day response for most complete enquiries
- Priority handling for urgent production problems
- Follow up support if the first cut needs adjustment
Pricing based on job complexity and support depth
Pricing is handled according to the amount of technical work needed. A straightforward parameter check for one tool and one material is priced differently from a full process review with multiple operations, tool life issues and production standardising. We keep the approach practical so you only pay for the support you actually need.
If the job leads to broader process changes, we can quote separately for application support or on site consultation. This is often the better option where a shop needs a repeatable setup for a steady production line, not just a single recommended speed and feed. Clear scope helps avoid surprises and keeps the work focused.
Keeping the settings right over time
Speed and feed settings are not a once off exercise. Tool wear, material batch changes, machine maintenance and operator changes can all shift the result. We recommend checking the critical numbers whenever a job changes material, tooling batch or holder length, and after any spindle, coolant or alignment issue.
For regular production, a monthly or job change review is usually enough for many shops. High volume work, tough materials or tight tolerance parts may need more frequent review. The aim is simple: protect the cutter, keep the finish consistent and reduce wasted machine time. Small adjustments early can save a lot of rework later.
Key facts
| Supported tools | Solid carbide end mills and drills |
|---|---|
| Typical diameters | 1 mm to 20 mm and selected sizes above, depending on application |
| Machine types | CNC machining centres, milling machines and drill tap units |
| Materials covered | Mild steel, stainless steel, cast iron, aluminium and alloy steels |
| Support format | Starting RPM, feed rate, chip load, depth of cut and engagement advice |
| Service area | Wadeville, Germiston plus Johannesburg, Pretoria, Cape Town, Durban and Gqeberha |